ARR Food Machines
ISO CERTIFIED MANUFACTURING

ARR Food Machines is a leading manufacturer of advanced conveyor systems, food processing machinery, and custom engineering solutions for modern industrial applications.

Trusted Engineering Partner
CORPORATE OFFICE
Plot No. 33, Road No. 6, Indra Complex Industrial Area, Tigaon Road, Kheri, Faridabad – 121002, INDIA
NAVIGATION

Request an Instant Quote / Inquiry

Share your requirement and our engineering team will get back to you shortly.

Multifloor Vertical Conveyors

Multifloor Vertical Conveyors

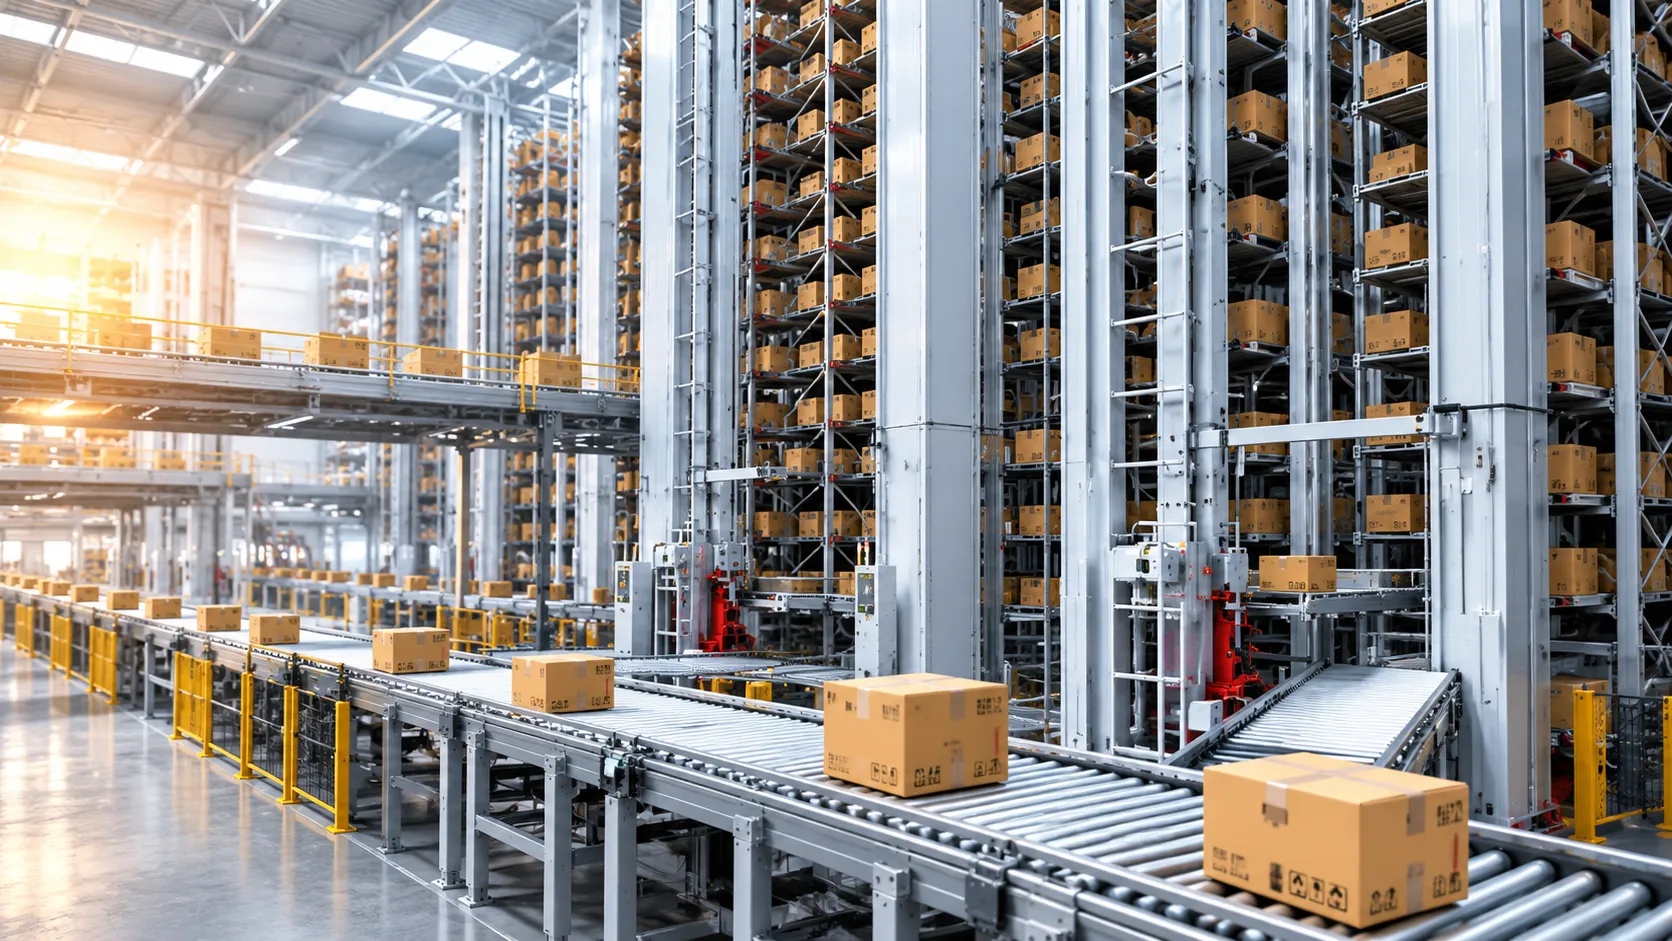
Multifloor Vertical Conveyors are designed to efficiently transport materials, cartons, boxes, crates, totes, and other goods between multiple floor levels in warehouses, manufacturing facilities, distribution centers, and industrial environments. These systems provide a reliable vertical material handling solution where horizontal conveyor systems or forklifts may require additional space and handling.

By utilizing vertical space, Multifloor Vertical Conveyors help optimize floor area while maintaining a smooth and organized flow of materials between different levels. The conveyor can be integrated with existing horizontal conveyor lines and automated material handling systems to create an efficient end-to-end conveying process.

Key Features

  • Multi-Level Material Transfer: Enables efficient movement of materials between multiple floors and working levels.
  • Space-Efficient Design: Makes effective use of vertical space while minimizing the required floor area.
  • Smooth Material Handling: Provides controlled and reliable movement of products between levels.
  • Flexible Configuration: Can be designed according to building layout, floor height, and material flow requirements.
  • Easy System Integration: Can be connected with horizontal conveyors and other material handling equipment.
  • Reduced Manual Handling: Helps minimize the need for manual transportation between different floors.
  • Industrial Construction: Designed for continuous operation in demanding industrial environments.
  • Safe & Controlled Operation: Supports stable and controlled vertical movement of conveyed materials.
  • Customized Solutions: Configuration can be adapted to suit different applications, capacities, and installation requirements.