ARR Food Machines
ISO CERTIFIED MANUFACTURING

ARR Food Machines is a leading manufacturer of advanced conveyor systems, food processing machinery, and custom engineering solutions for modern industrial applications.

Trusted Engineering Partner
CORPORATE OFFICE
Plot No. 33, Road No. 6, Indra Complex Industrial Area, Tigaon Road, Kheri, Faridabad – 121002, INDIA
NAVIGATION

Request an Instant Quote / Inquiry

Share your requirement and our engineering team will get back to you shortly.

Conveyor

Continuous Vertical Chain Conveyor

A Continuous Vertical Chain Conveyor is an advanced material handling solution designed to transport cartons, boxes, crates, trays, totes, and lightweight pallets efficiently between multiple floor levels. Using a robust chain-driven lifting mechanism, it provides continuous vertical movement while ensuring smooth, safe, and uninterrupted product flow throughout the facility.

Ideal for warehouses, distribution centers, manufacturing plants, e-commerce fulfillment centers, food processing units, and pharmaceutical industries, this vertical conveyor maximizes floor space, reduces manual handling, and integrates seamlessly with automated conveyor systems. Its compact design, reliable performance, and low maintenance requirements make it a cost-effective solution for improving productivity and streamlining warehouse automation.
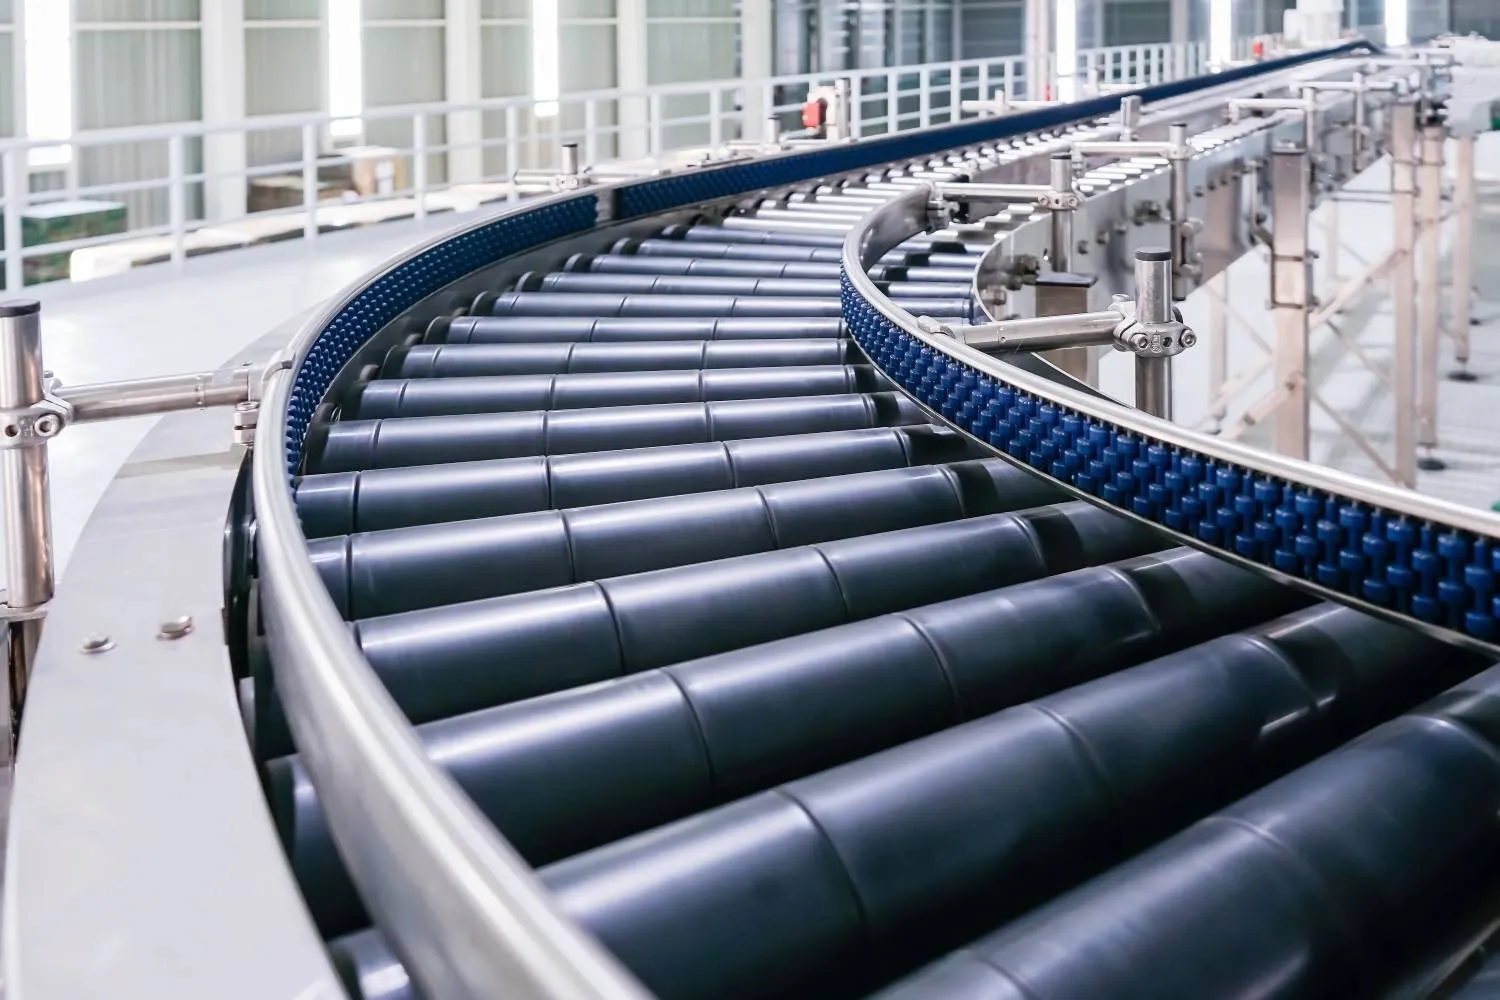
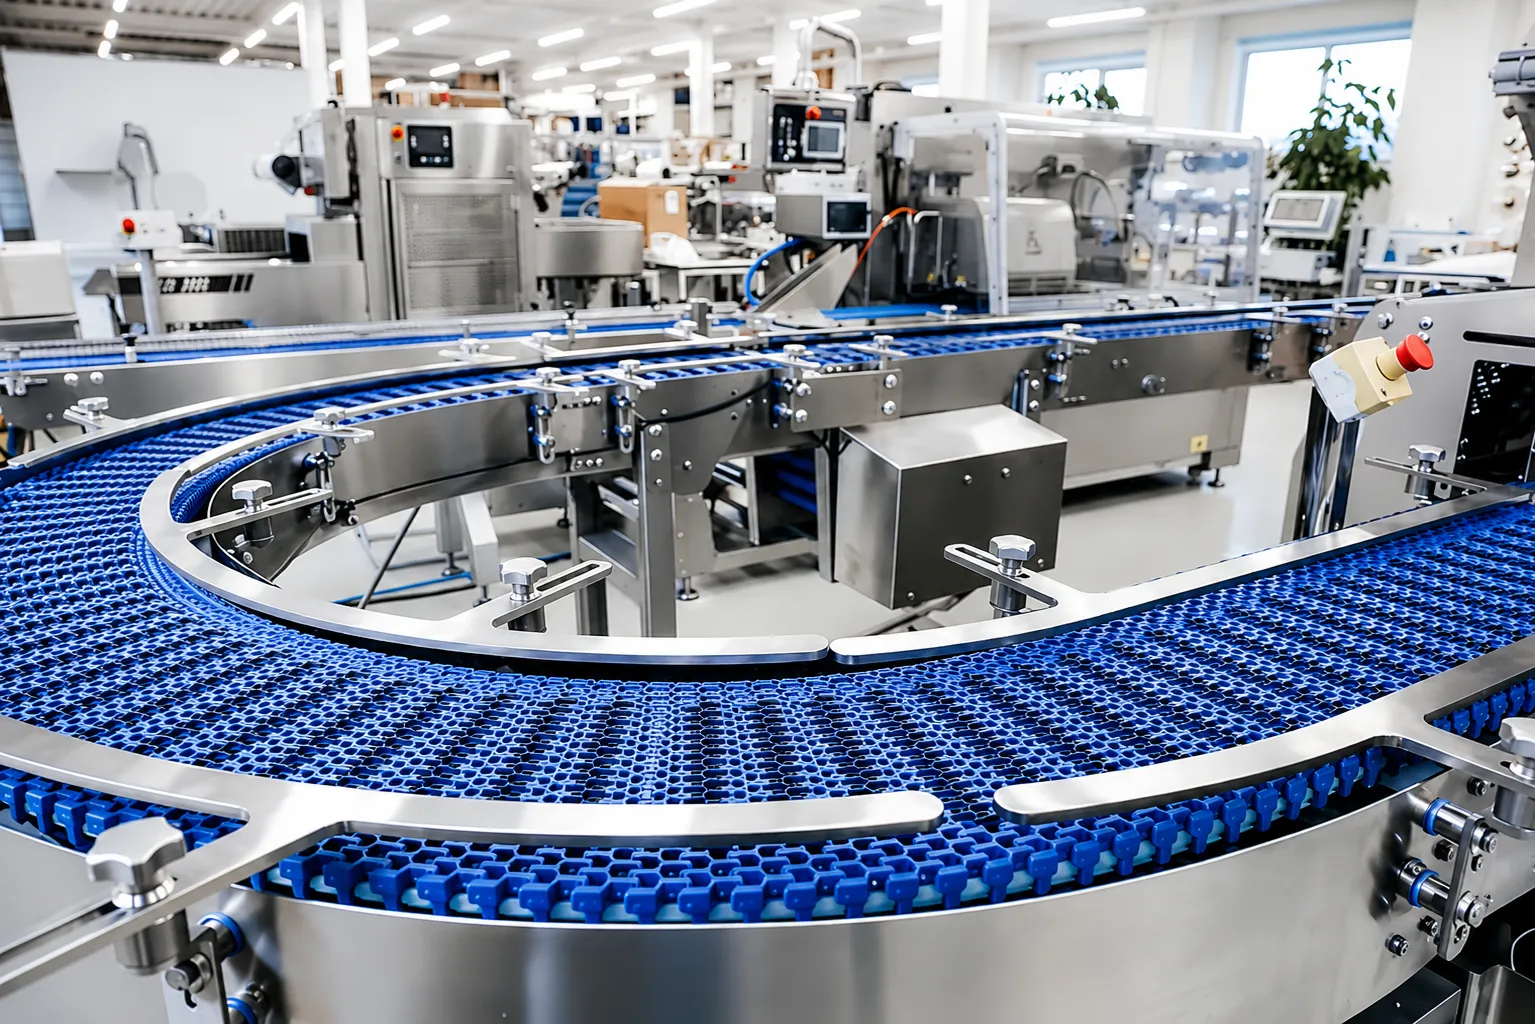
Key Benefits of Continuous Vertical Chain Conveyors

  • Space-Saving Design: Utilizes vertical space efficiently, saving up to 60% of valuable floor area.
  • Continuous Product Flow: Enables uninterrupted movement of cartons, boxes, crates, trays, and pallets between different floor levels.
  • High Throughput: Handles large volumes of products quickly, improving operational efficiency.
  • Smooth & Safe Transportation: Minimizes product damage with stable and controlled vertical movement.
  • Easy System Integration: Seamlessly connects with conveyors, sortation systems, ASRS, and other warehouse automation solutions.
  • Reduced Manual Handling: Eliminates manual lifting, improving workplace safety and reducing labor costs.
  • Reliable Heavy-Duty Construction: Built for continuous industrial operation with minimal maintenance requirements.
  • Improved Warehouse Productivity: Accelerates material flow, reduces bottlenecks, and increases order processing speed.
  • Versatile Industrial Applications: Suitable for logistics, e-commerce, manufacturing, food processing, pharmaceuticals, automotive, and packaging industries.
  • Energy-Efficient Performance: Optimized drive system delivers reliable operation with lower power consumption.